Discontinuous Dense Phase System for Fly Ash Handling – Cement Industry, Tamil Nadu
Reliable, continuous fly ash handling is critical for cement manufacturers, where unplanned downtime or manual bottlenecks can ripple straight into production.
Discontinuous Dense Phase Conveying System for Filter Aid/Pre-coat Material & Lime/Sulphur Powder
Handling low-bulk-density filter aid and pre-coat material alongside reactive lime and sulphur powder calls for a conveying technology that protects product quality
Lean Phase Positive Pressure System for PET Flakes
Efficient handling of lightweight PET flakes require a conveying system that can maintain high transfer rates while ensuring gentle material handling and reliable distribution
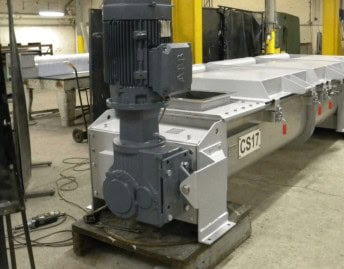
Discontinuous Dense Phase System for Iron Ore/Pellet Dust Conveying
Efficient handling of iron ore and pellet dust is a critical requirement in steel manufacturing facilities, particularly when materials
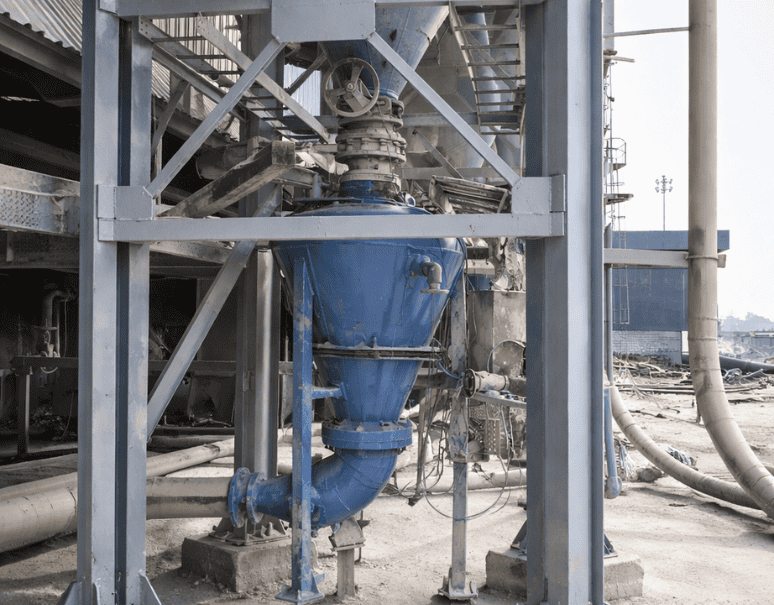
Discontinuous Dense Phase System for Foundry Sand Conveying
Efficient reclaimed sand handling is essential for maintaining productivity and process continuity in foundry operations.
Discontinuous Dense Phase System for Fly Ash Conveying & Wet Ash Unloading System
Macawber Engineering Systems India Pvt. Ltd successfully executed a complete fly ash handling and wet ash unloading system
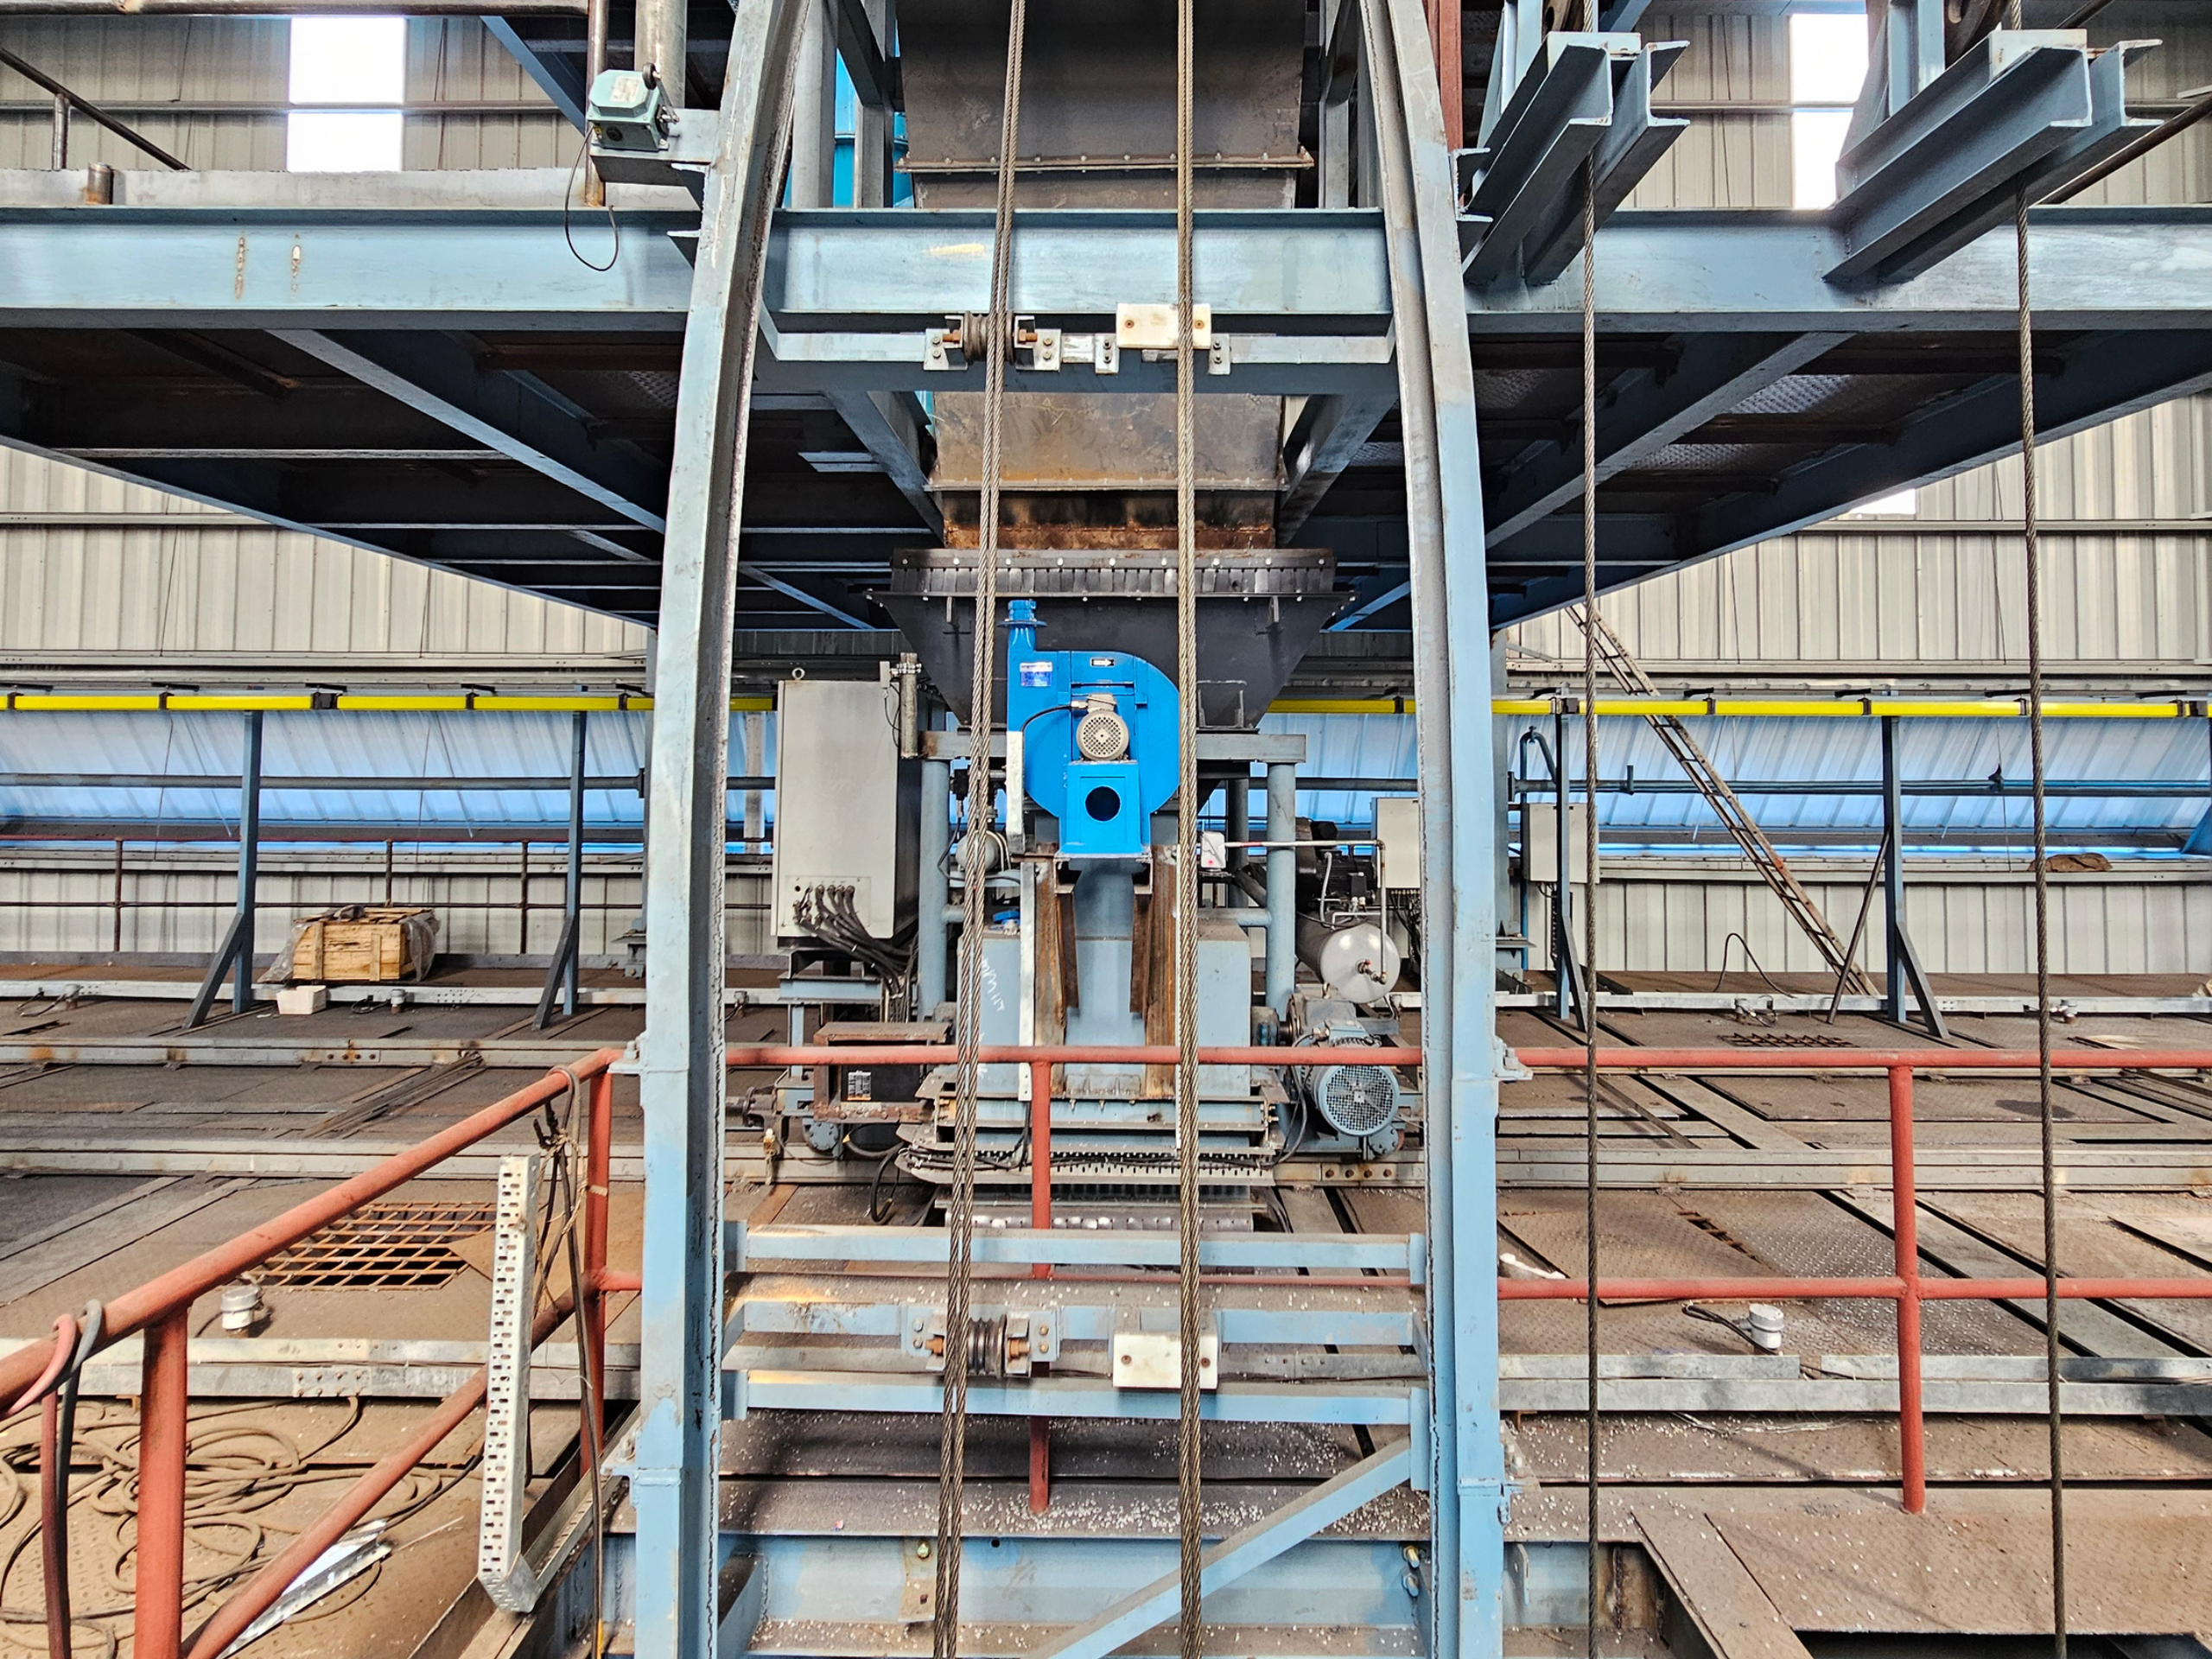
Pneumatic Conveying, Storage, Batching, Weighing For Graphite & Other Dust
This case study features Macawber India, the top pneumatic conveying system manufacturer, rolling out a cutting-edge
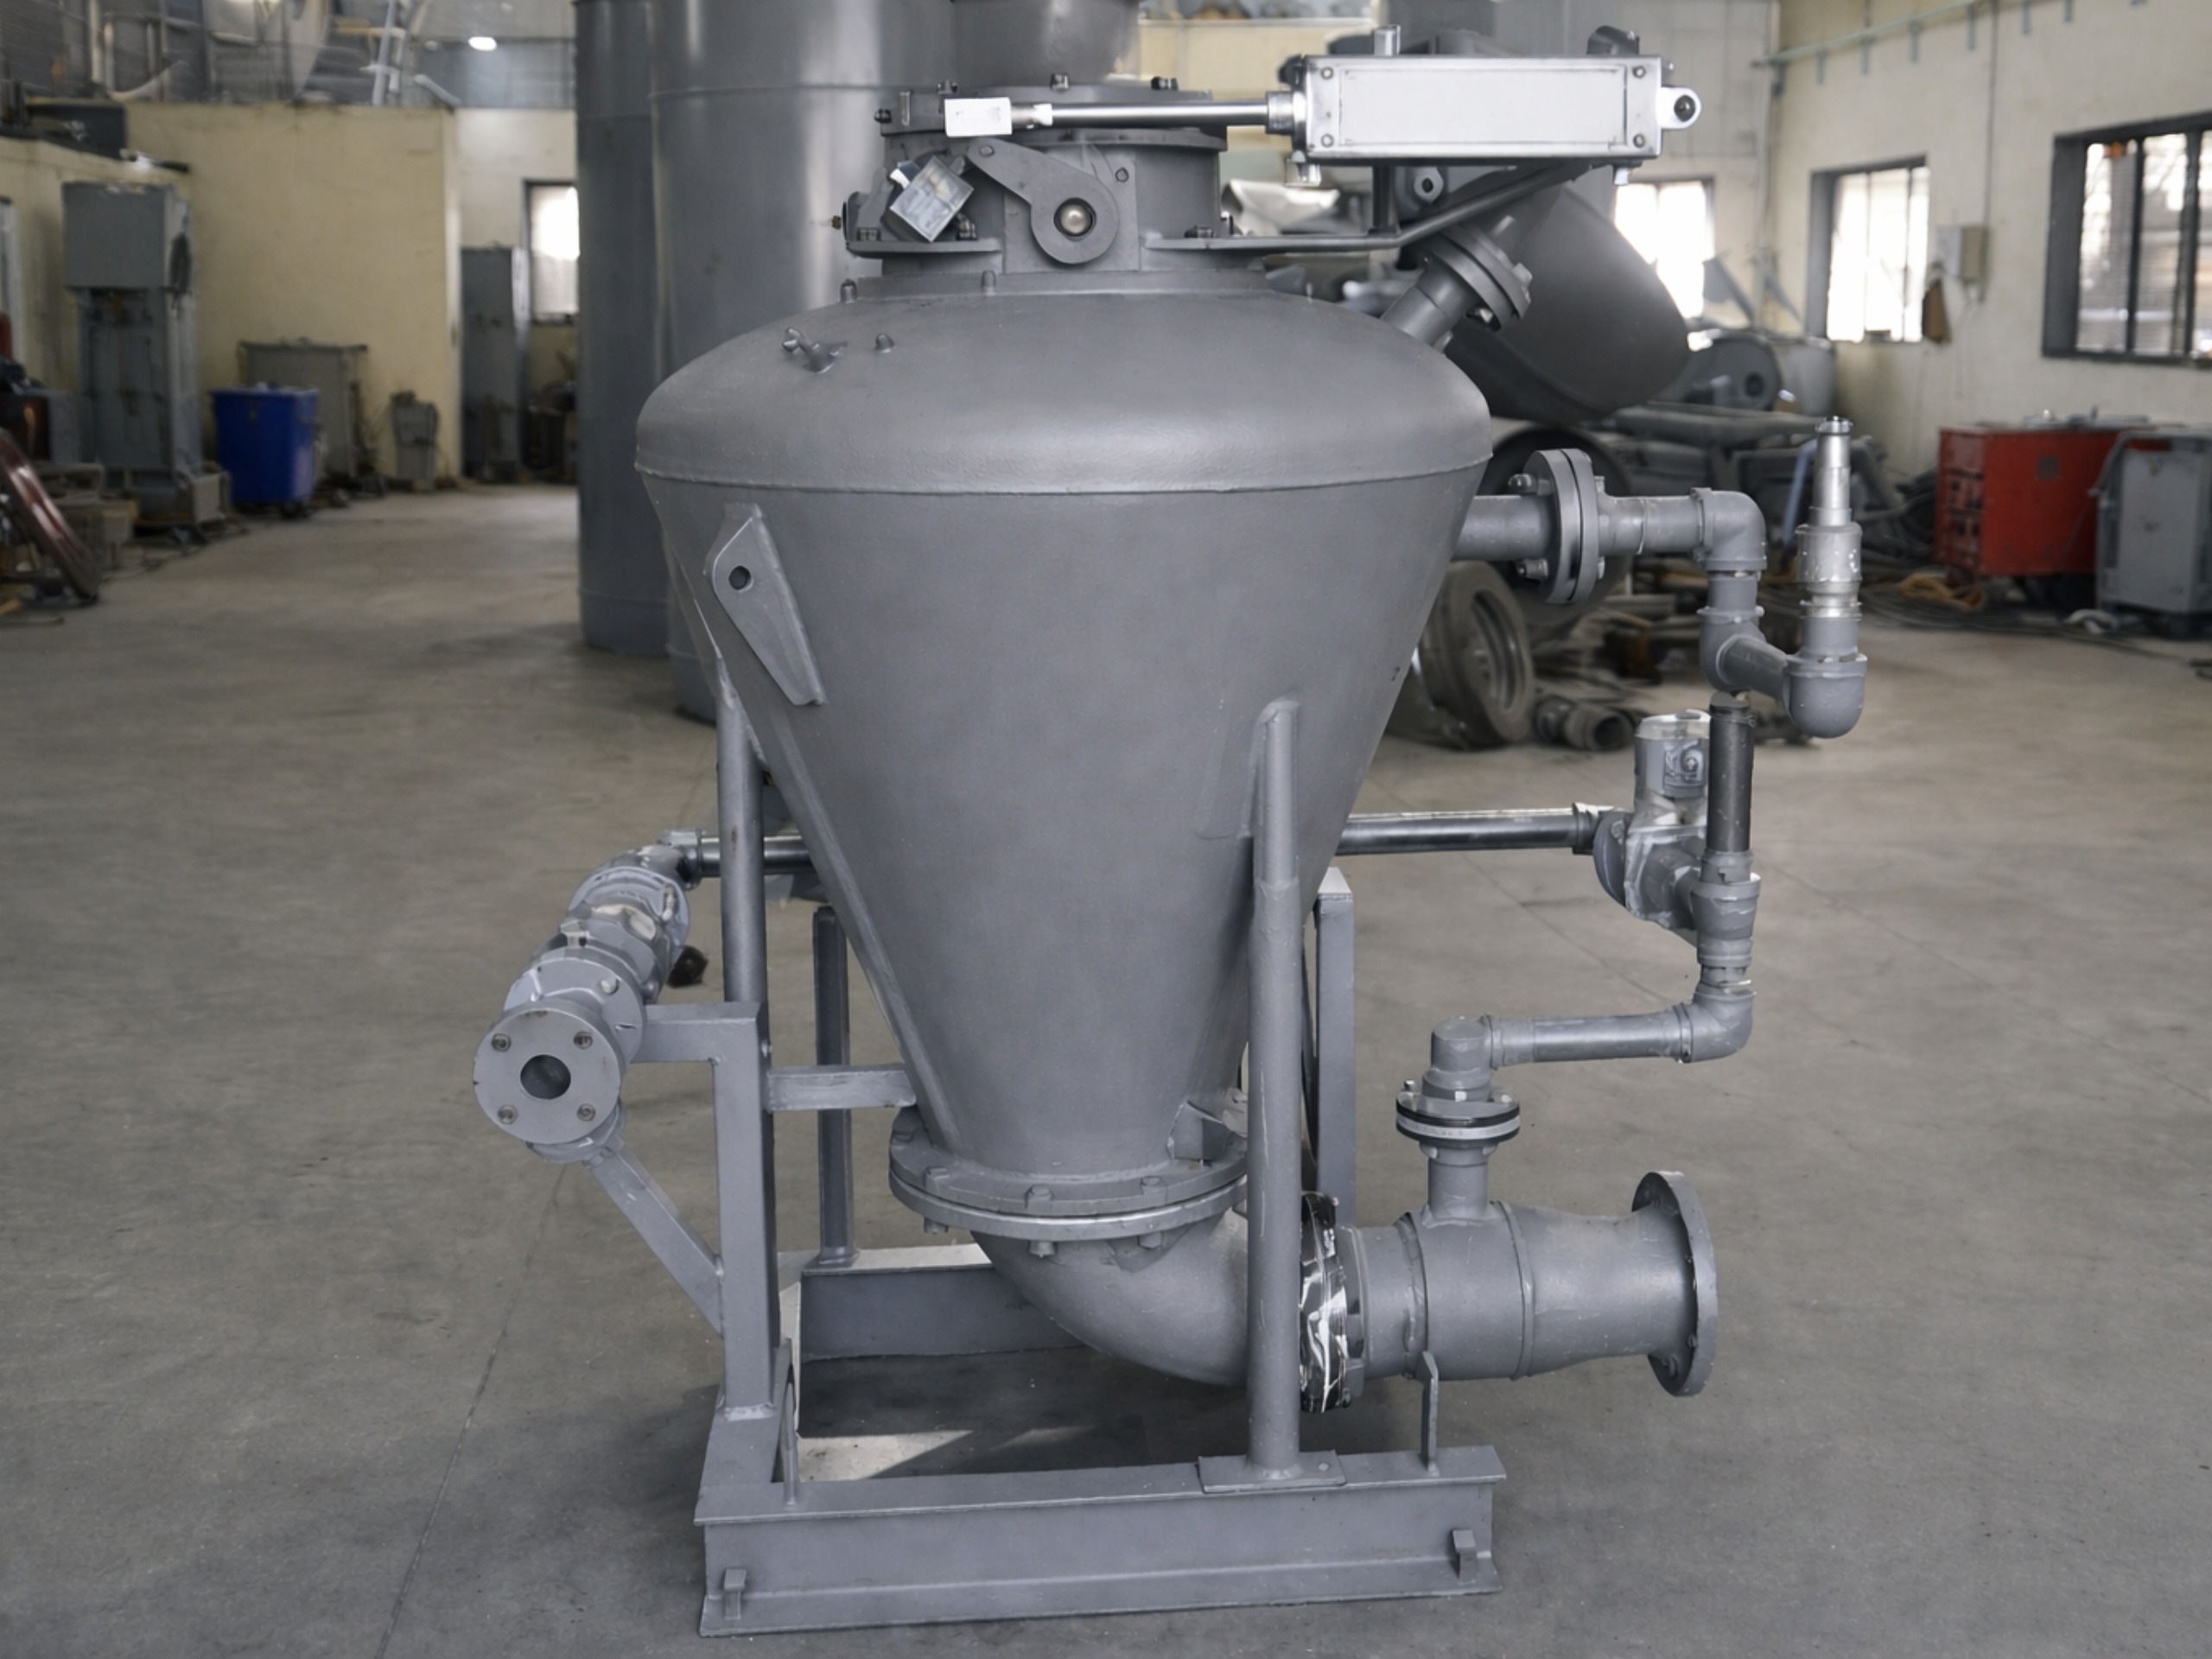
Discontinuous Dense Phase System For Coffee & Chicory
Macawber India was selected to create a unique Dense Phase Pneumatic Conveying System. It makes use of advanced diverter valves to control
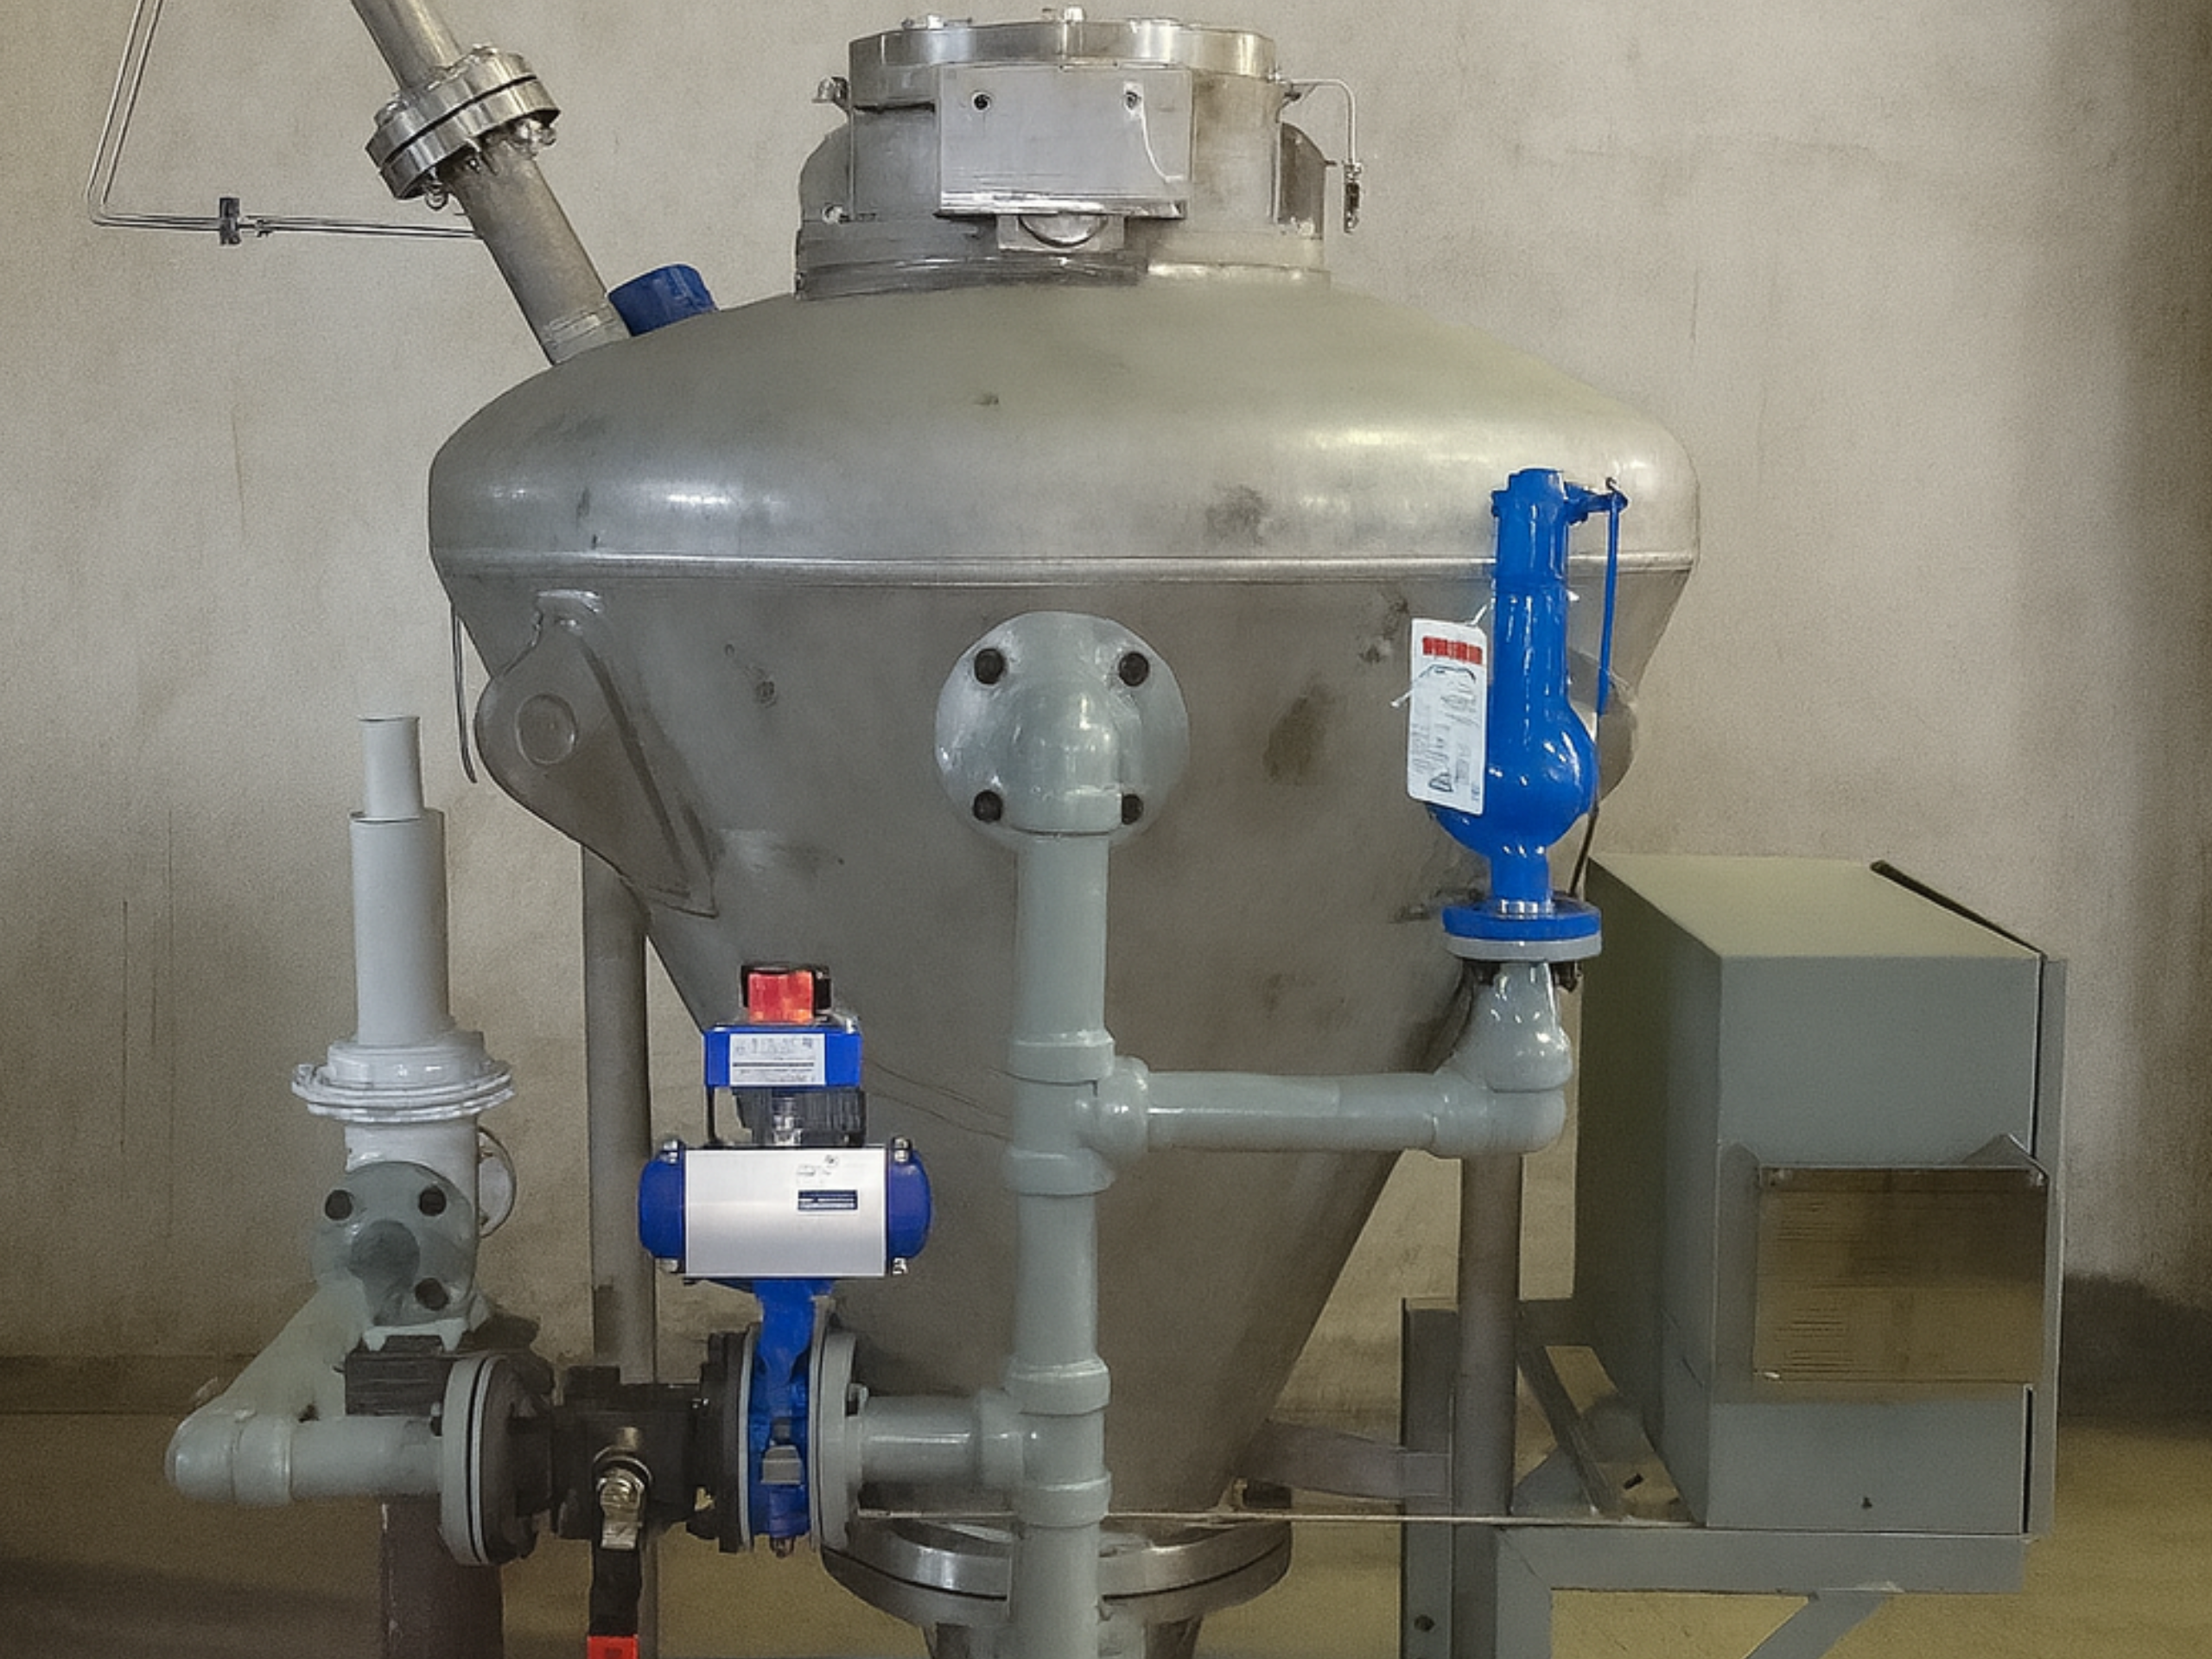
Discontinuous Dense Phase System for Optical Brightener
The following case study highlights Macawber India, the leading pneumatic conveying system manufacturer
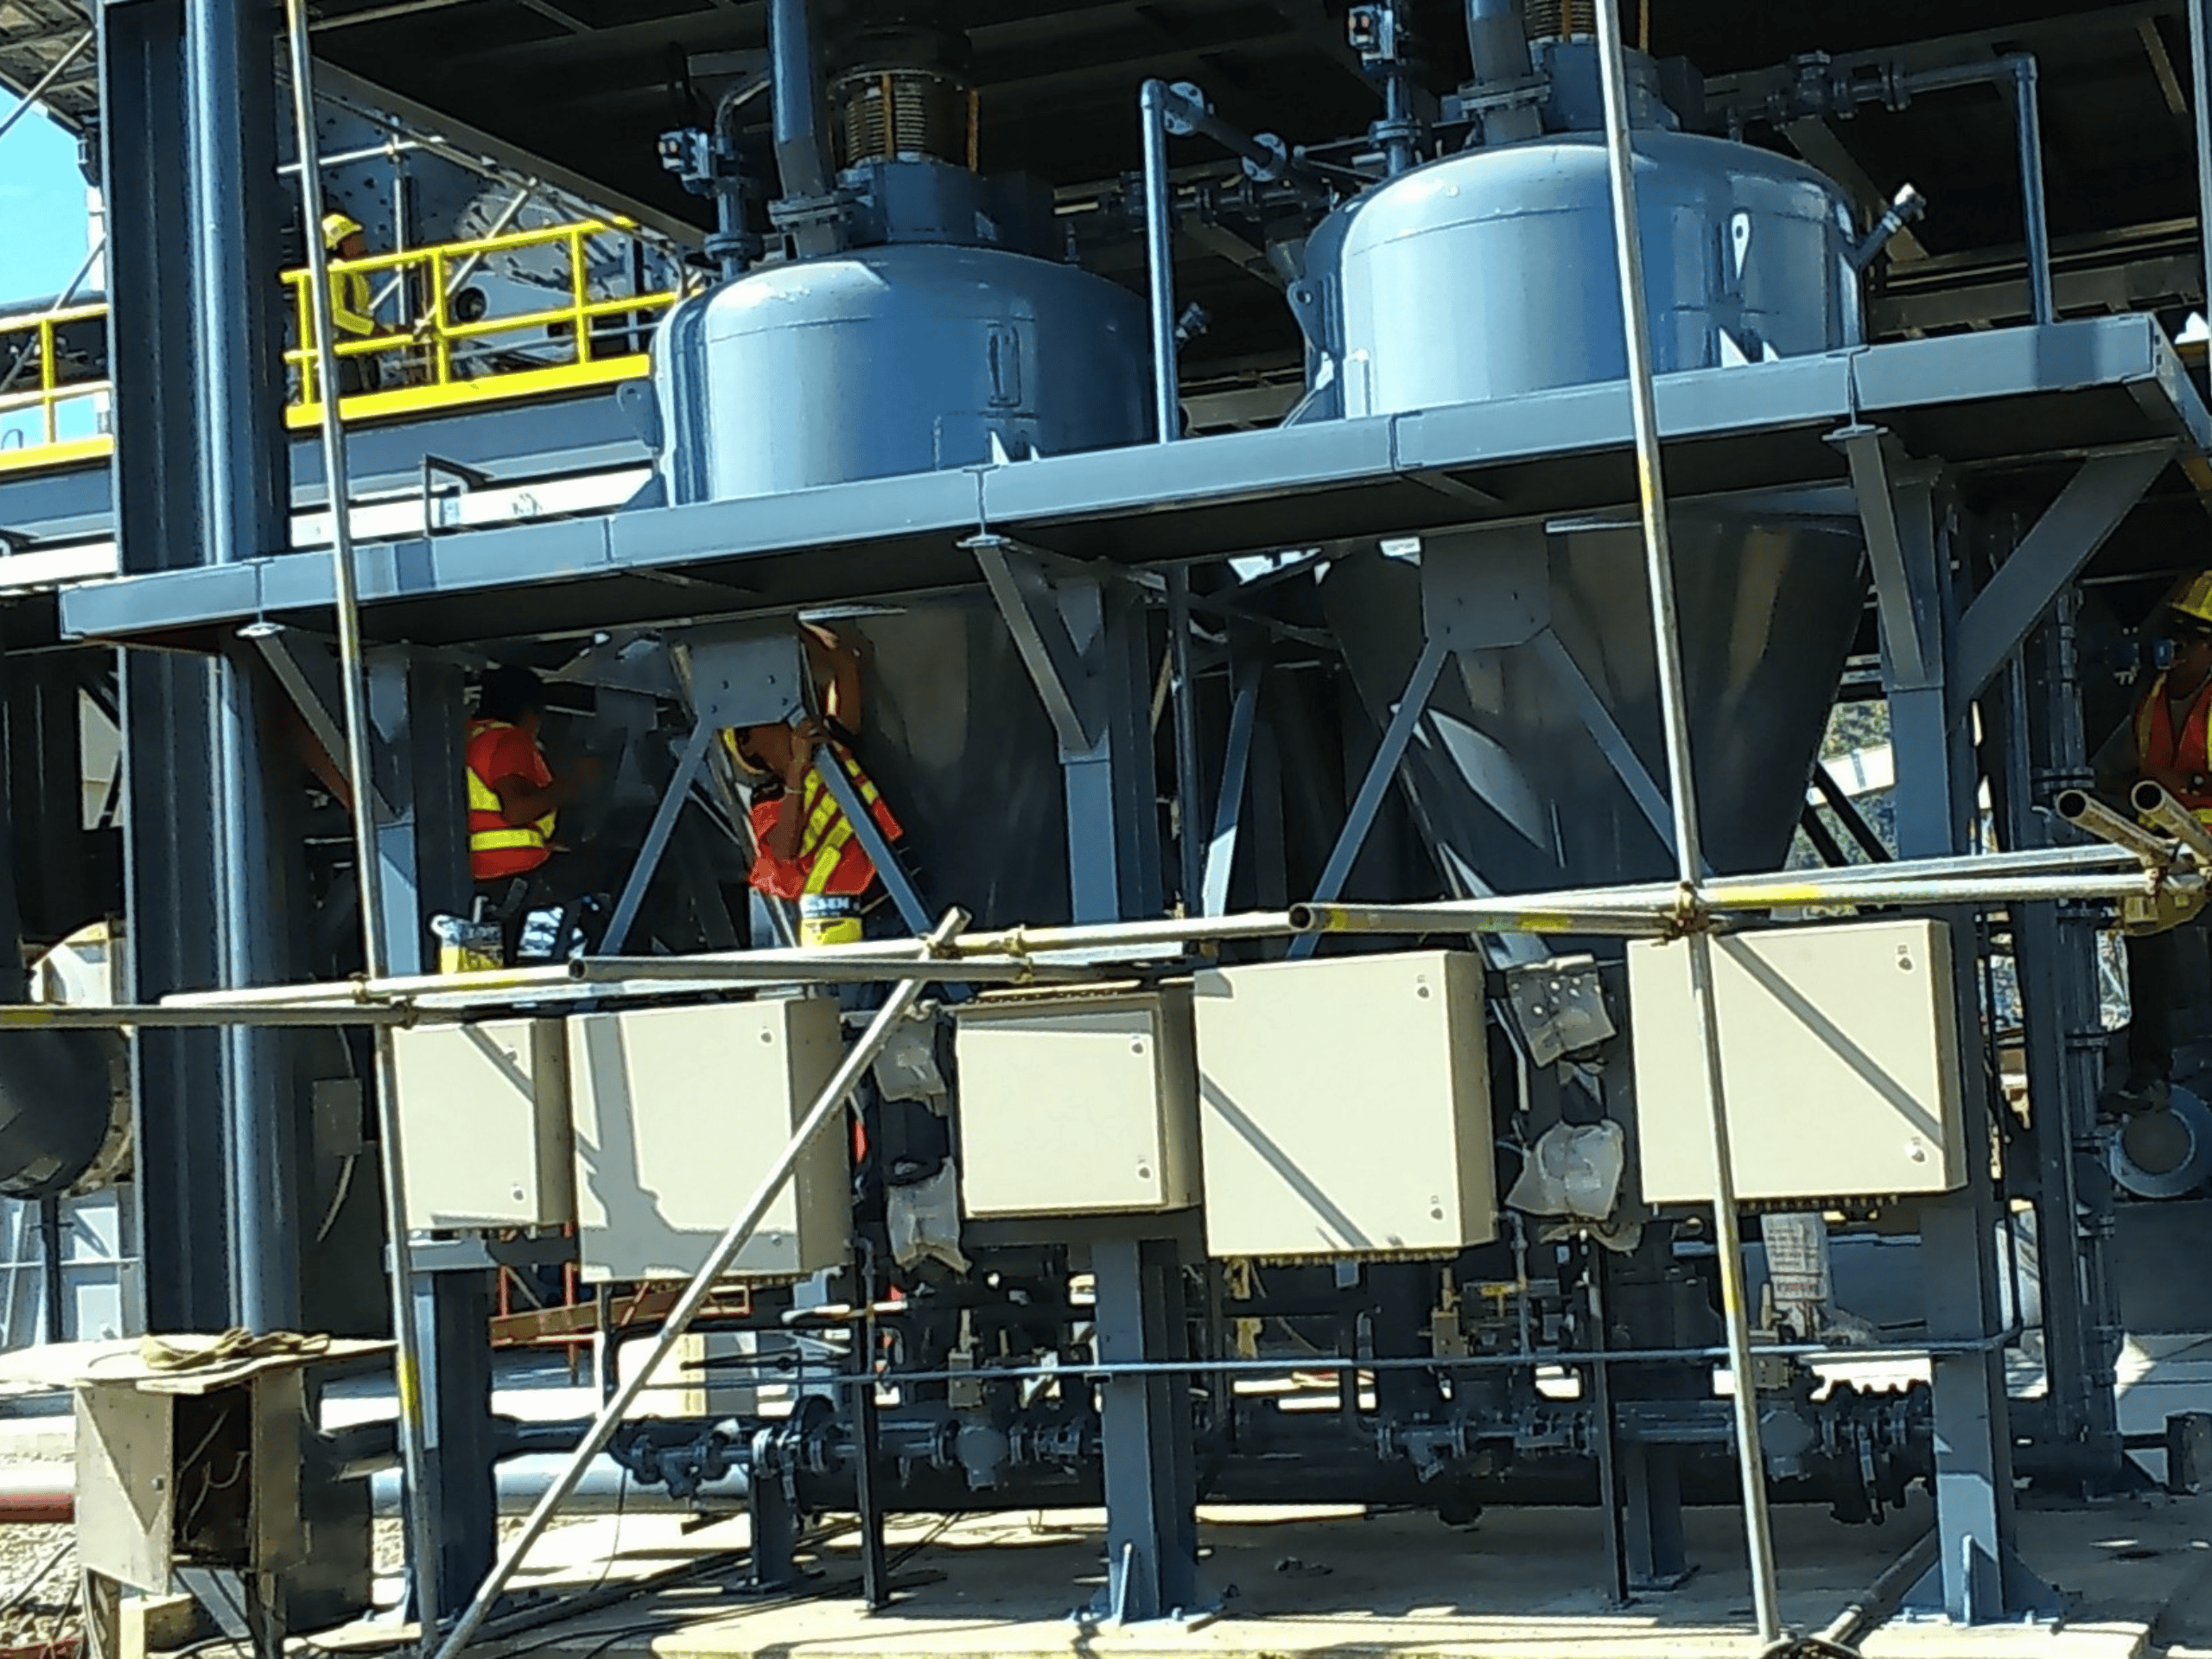
Discontinuous Dense Phase System For Calcined Lime – Power Plant, Philippines
This case study focused on our customer, who is one of the leading power companies in the Philippines.
Gentle and Dust-Free Conveying of PET Chips for SRF’s BOPET Film Line
Our customer, a leader in packaging films, wanted a safe, efficient, and contamination-free material handling system
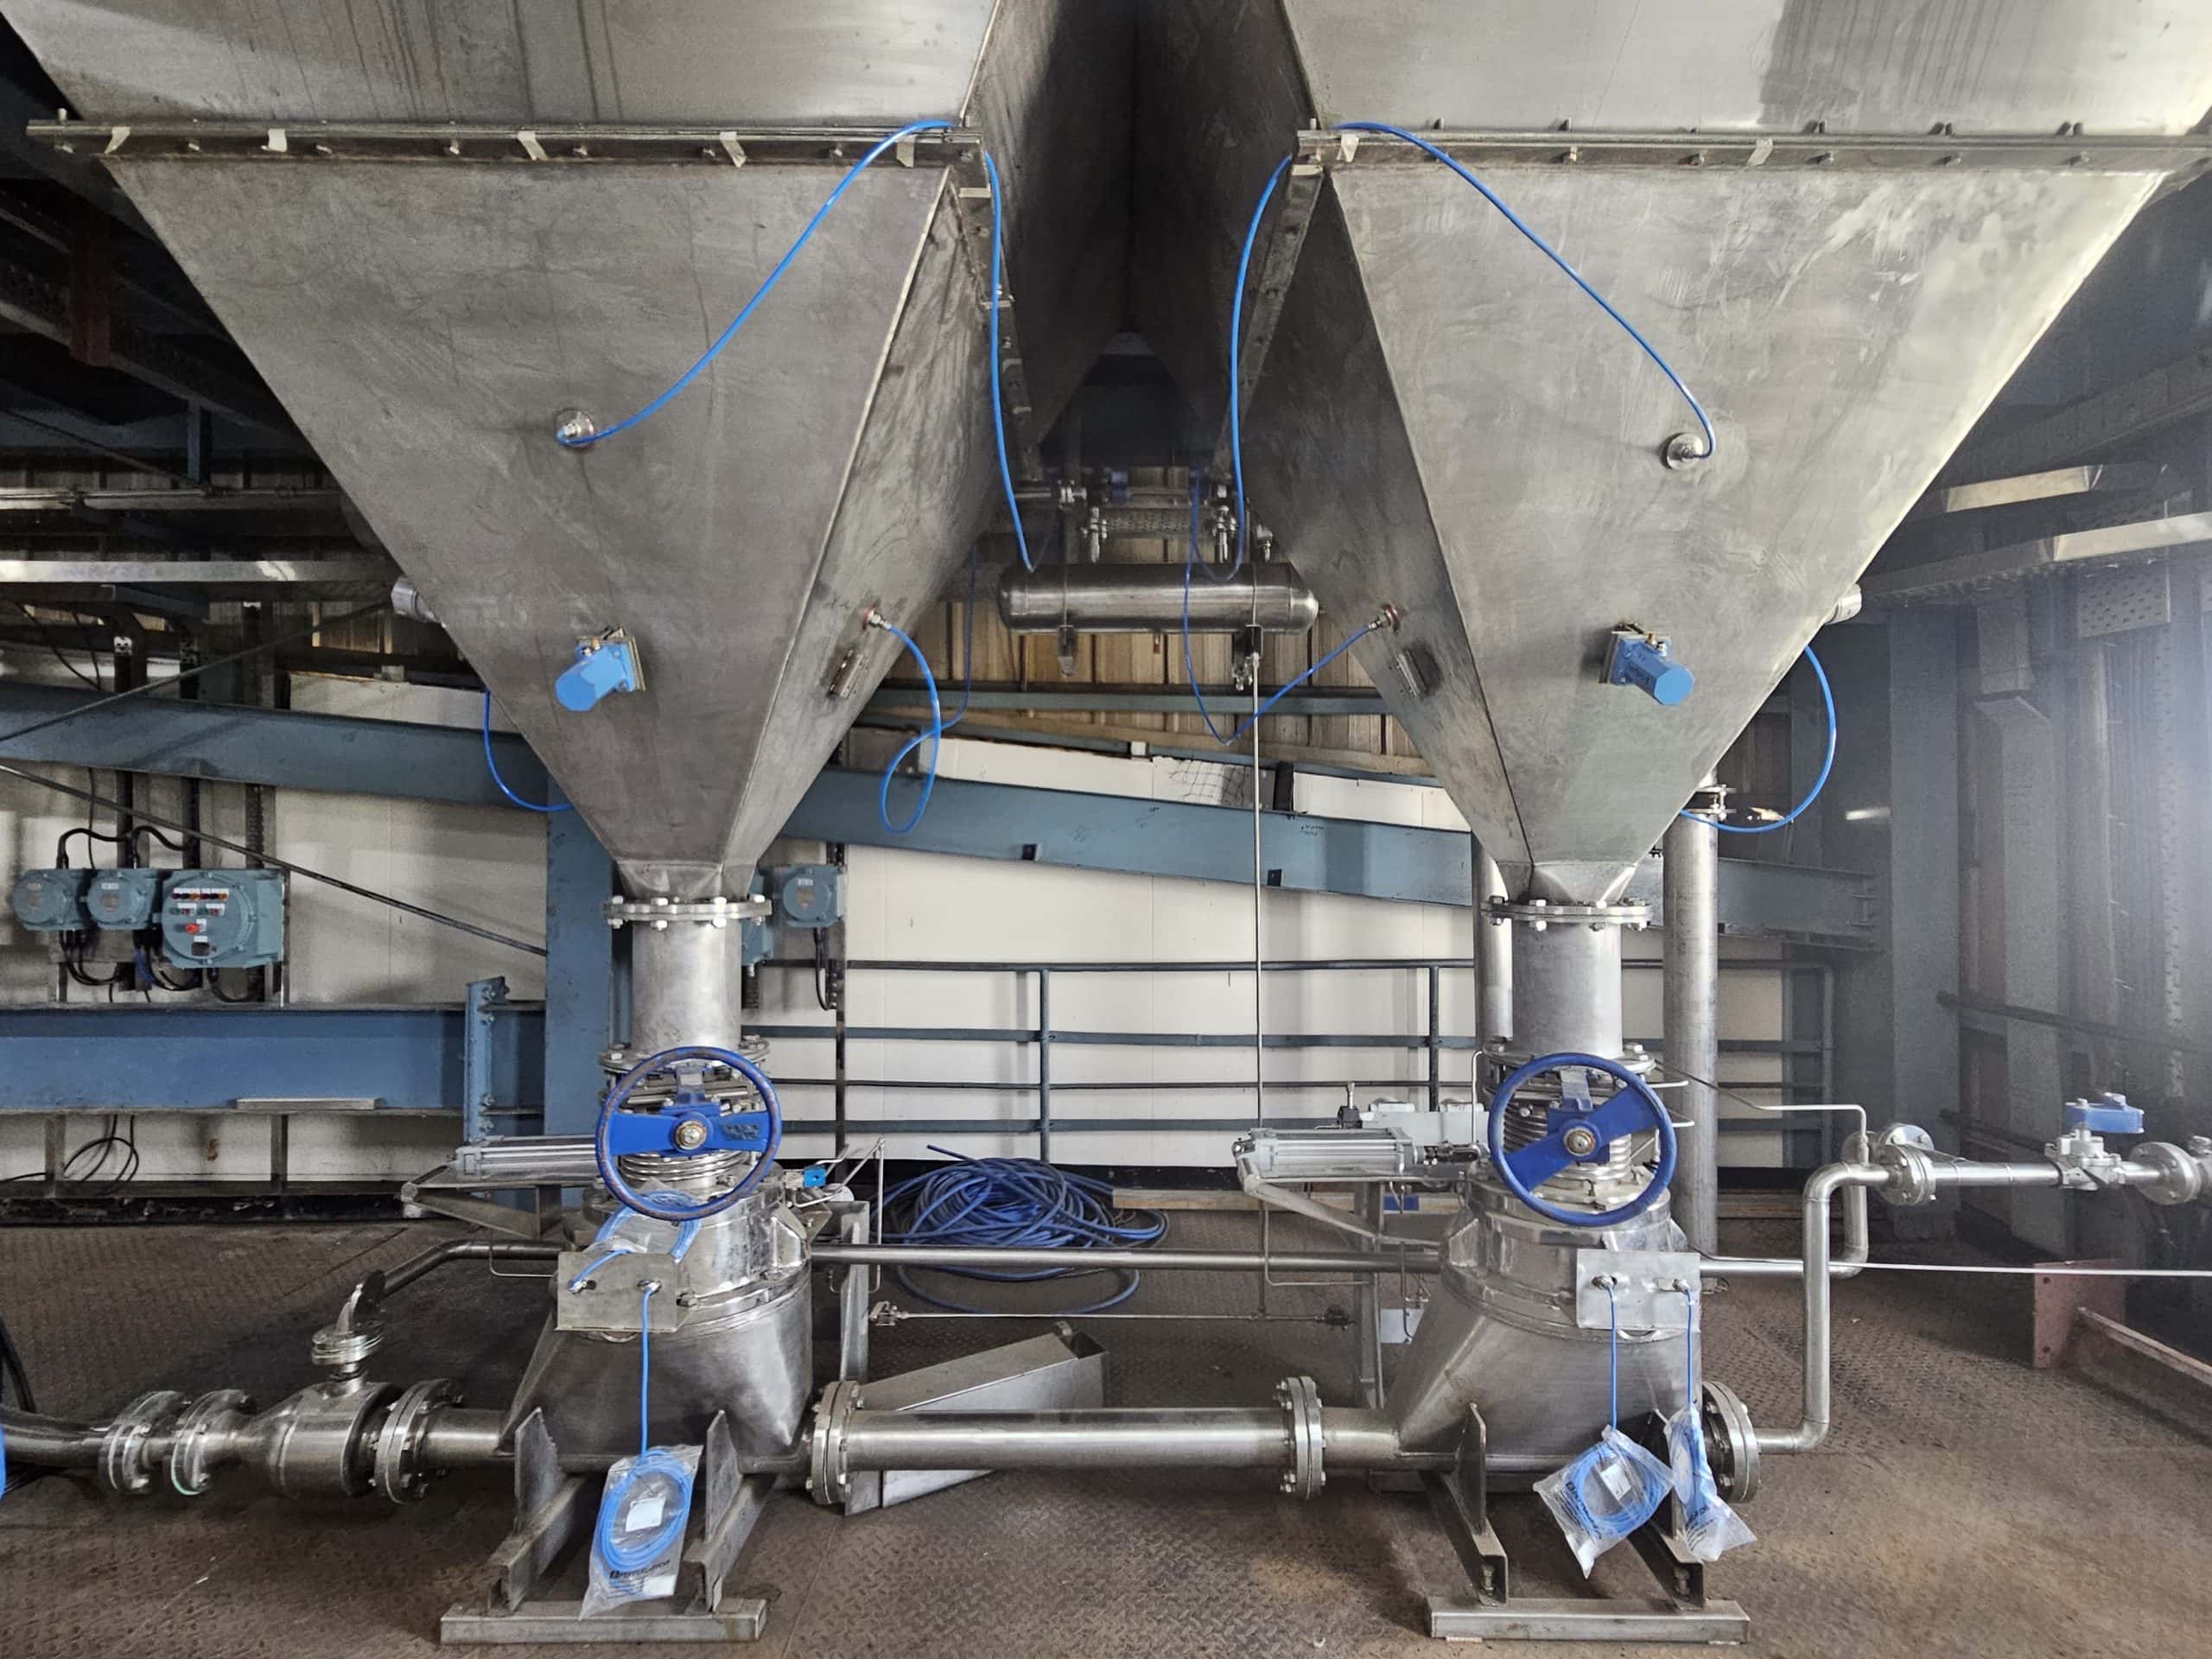
Pneumatic conveying, batching & weighing system for Talc
The customer needed an integrated material handling solution for talc powder at their soap factory in Uttarakhand.
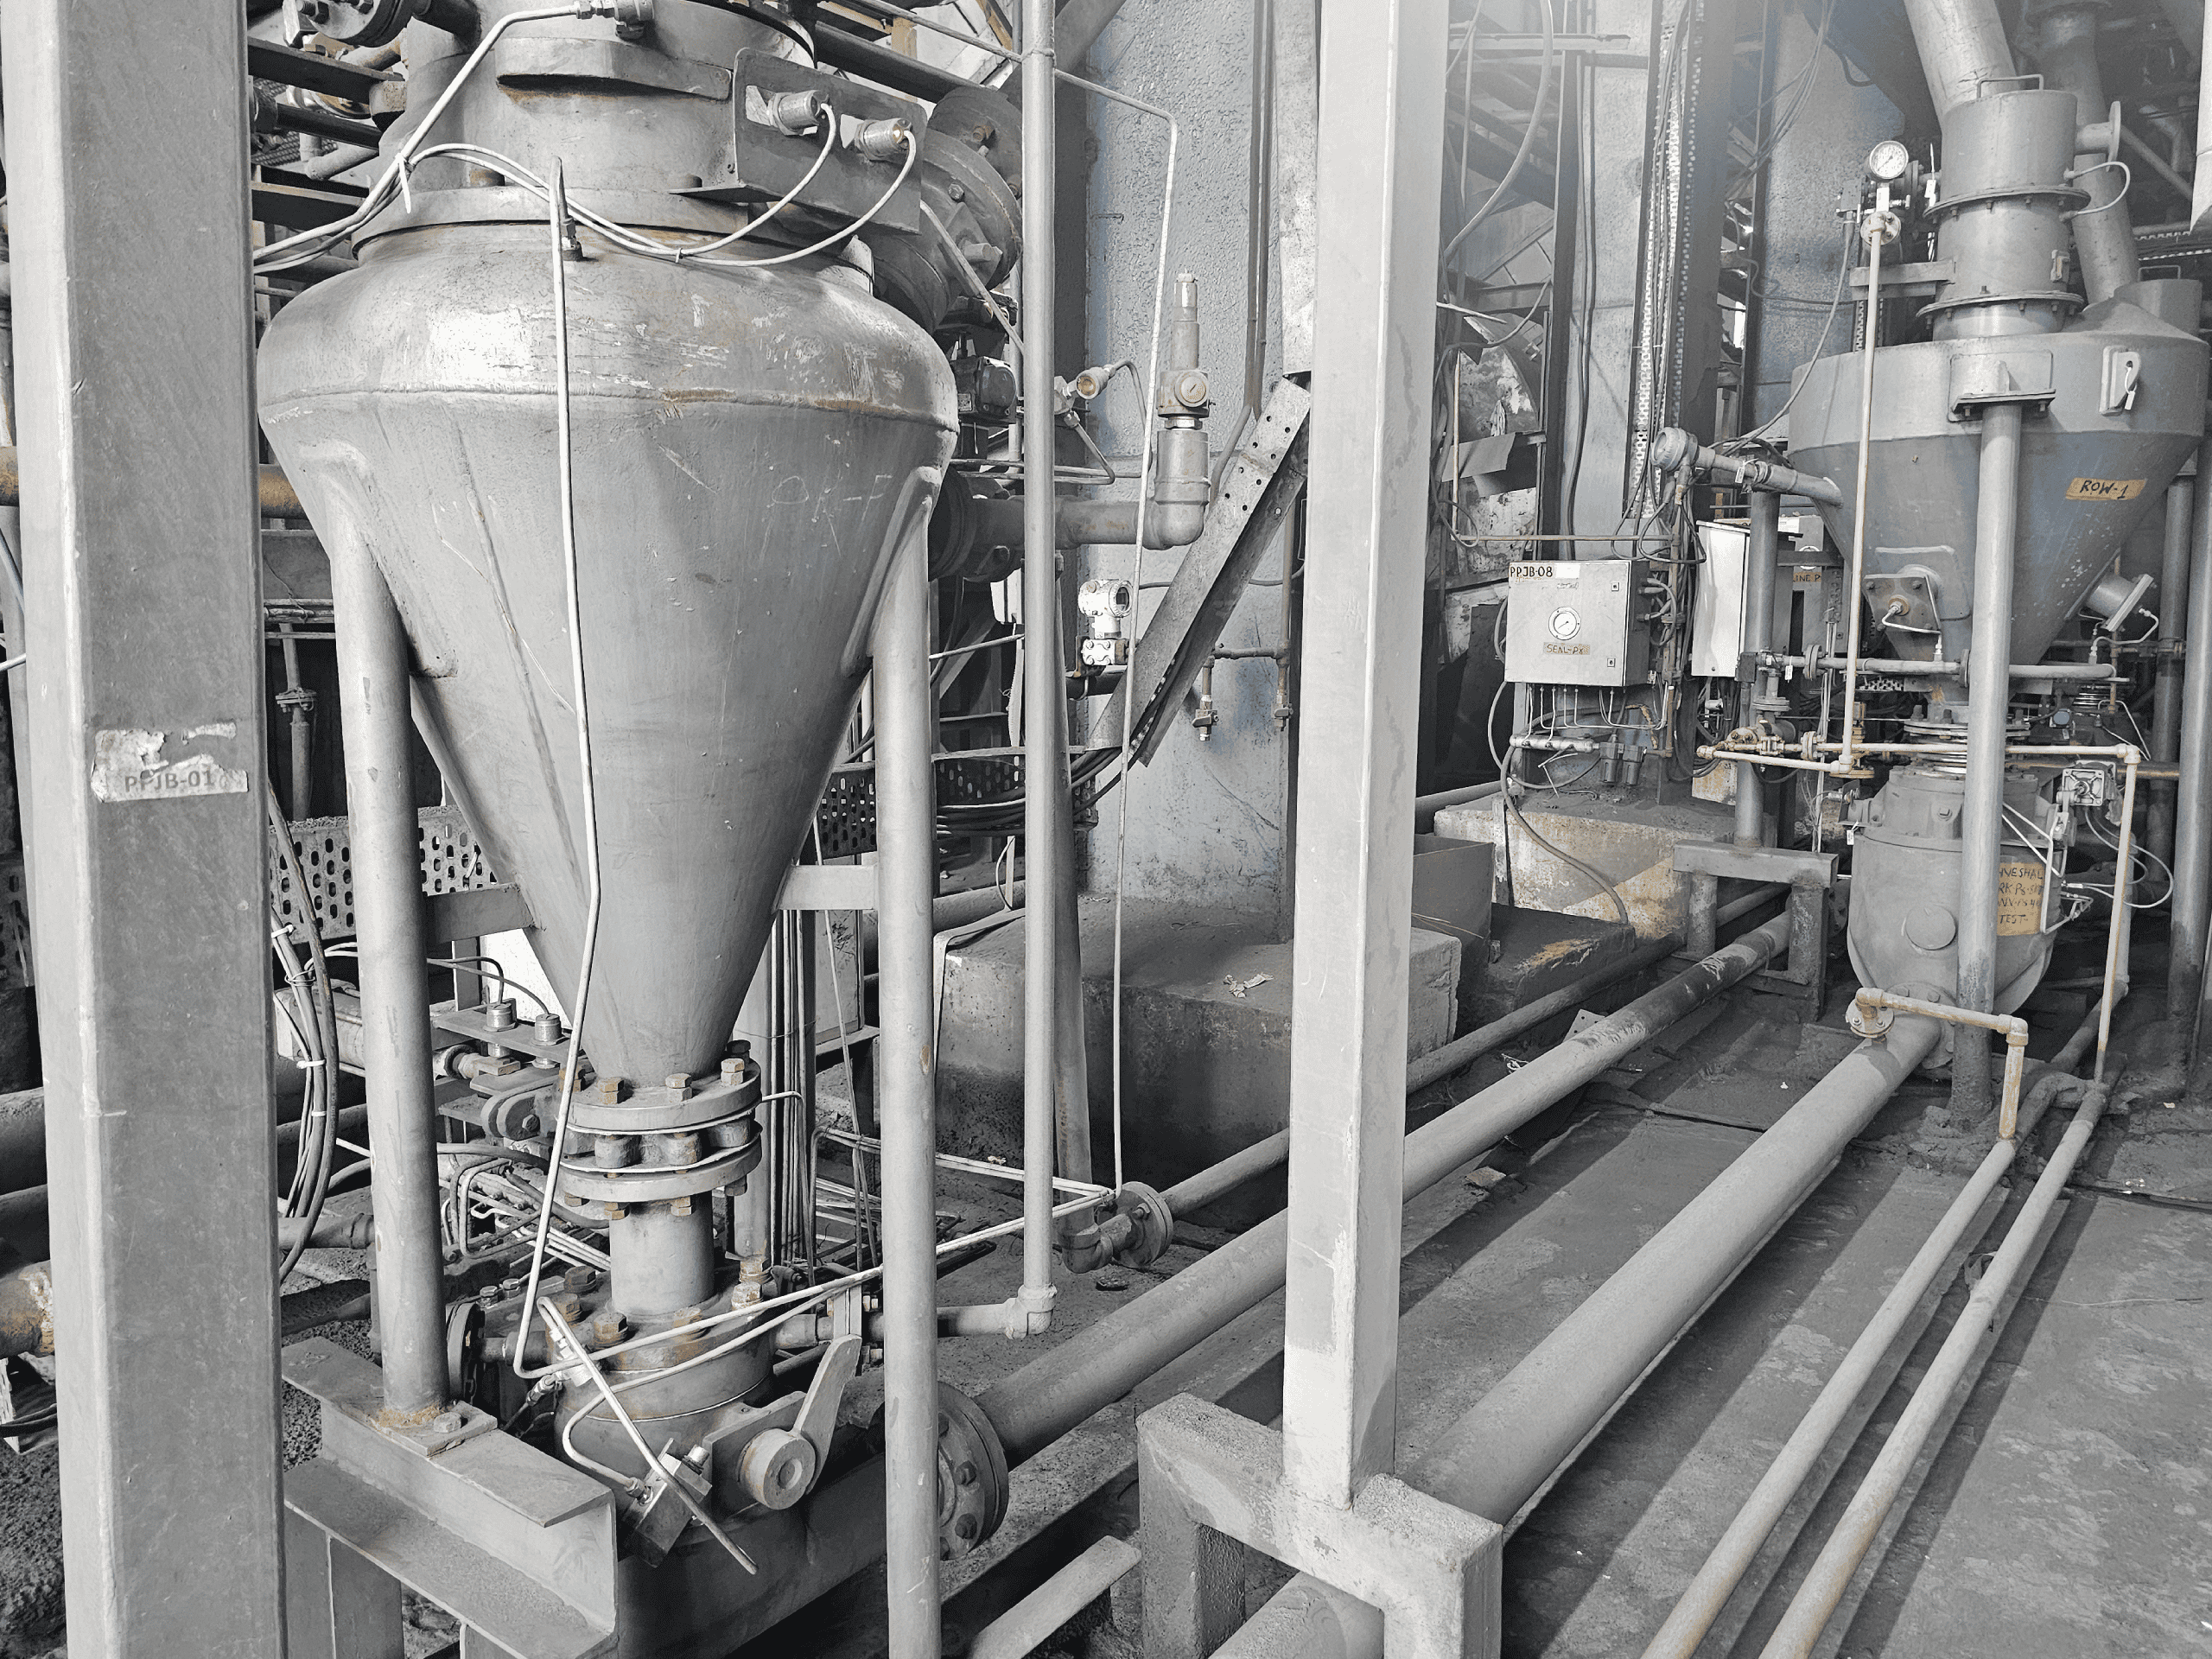
Safe Handling of Coke Oven Dust with Nitrogen-Based Dense Phase Pneumatic Conveying
The customer required a safe and reliable coke oven dust handling solution for the dust, which accumulated in the mill fan section.